LYNCCN CNC grinding workshop
HomeProductsAmada StyleAmada Style Sash Punch 88° R0.6 H120mm

Amada Style

A sash punch with 120 mm useful height for Amada-type press brakes, machined from 42CrMo, heat treated and precision ground. Rated up to 35 tons per metre.

Amada Style Sash Punch 88° R0.6 H120mm

A sash punch with 120 mm useful height for Amada-type press brakes, machined from 42CrMo, heat treated and precision ground. Rated up to 35 tons per metre.

Tool system
Amada system
Length
835 / 415 / 835 seg. / 805 seg. mm
Total height
150 mm
Height
120 mm
Thickness
26 mm
Angle
88°
Radius
0.6 mm
Max. load
35 T/m
Steel
42CrMo
Making time
25–30 days
Package
Wooden crate
  • 42CrMotool steel
  • 25–30 daysmaking time
  • Wooden cratepacking
Product information

42CrMo Steel, Hardened
Where the Tool Works

The whole body is heat treated for strength and toughness, then the working area is hardened again for wear resistance — a strong body with a hard, durable tip.

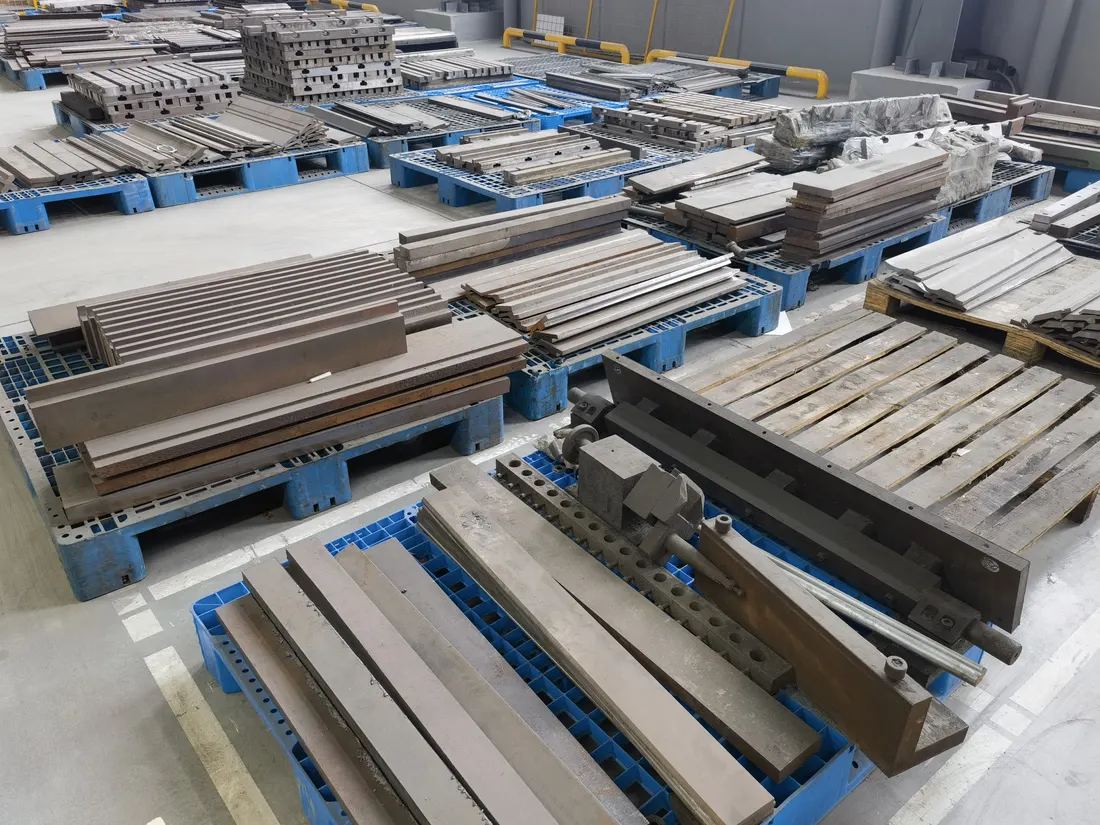
Heat treated press brake tool blanks in the LYNCCN workshop

Heat treated tools before precision grinding

Full-body heat treatment

HRC 50± 2 Through the whole tool body

Induction hardening

HRC 54± 2
05 mm
Depth 3–4 mm

Laser hardening

HRC 54± 2
05 mm
Depth 1–1.5 mm
  • Material42CrMo alloy steel
  • Surface treatmentSand blasting / blackening
  • Making time25–30 days
  • PackageWooden crate, soft film layers inside

01Product Introduction

The LS10.20 is a sash punch for Amada-type press brakes. A 120 mm useful height, 26 mm body, 88° tip and 0.6 mm radius reach tall flanges, at up to 35 tons per metre.

It is machined from 42CrMo alloy steel, full-body heat treated to HRC 50 ± 2, hardened again on the working area and precision ground. Order it in 835 or 415 mm lengths, or as an 835 or 805 mm segmented set when you need to bend boxes and short flanges.
02Product Advantages

  • Made for Amada-type clamping

    Amada system tang, standard 835 / 415 mm lengths and segmented 835 / 805 mm sets for press brakes with Amada-type upper clamps.

  • Tough 42CrMo alloy steel

    A chromium-molybdenum steel chosen for strength under load — up to 35 T/m for this profile.

  • Hardened where it wears

    Full-body heat treatment HRC 50 ± 2, plus induction (HRC 54 ± 2, 3–4 mm) or laser hardening (HRC 54 ± 2, 1–1.5 mm) on the working area.

  • Precision ground

    Working surfaces are ground on CNC grinders for consistent angles from one tool to the next.

  • Protected surface and packing

    Sand blasted / blackened surface; shipped in a wooden crate with soft film layers inside.

  • Other variants on request

    Different angle, radius, height, length or your own drawing — we machine the tool to your specification.

03Technical Parameters

ModelLS 10.20.0
Tool systemAmada system
Length835 / 415 / 835 seg. / 805 seg. mm
Total height150 mm
Useful height120 mm
Thickness26 mm
Steel type42CrMo
Tonnage35 T/m max.
Angle88°
Radius0.6 mm
Heat treatmentFull-body HRC 50 ± 2 · induction HRC 54 ± 2 (depth 3–4 mm) · laser HRC 54 ± 2 (depth 1–1.5 mm)
Surface treatmentSand blasting / blackening
Making time25–30 days
PackageWooden crate with soft film layers inside
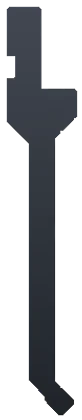
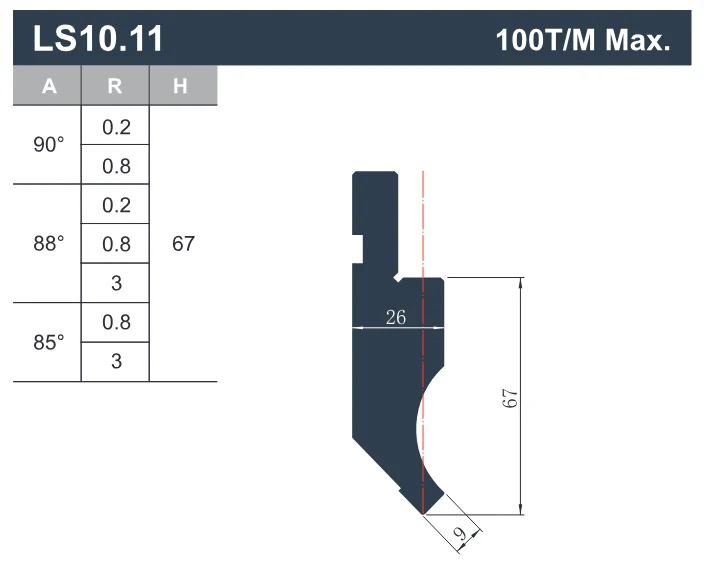
LS10.11 profile drawing with dimensions

This profile

AngleRadiusH
88°R0.6120

Standard segmentation (Amada style)

835 mm 8 segments

  1. 10
  2. 15
  3. 20
  4. 40
  5. 50
  6. 100
  7. 200
  8. 400

805 mm 8 segments

  1. 10
  2. 15
  3. 20
  4. 40
  5. 50
  6. 100
  7. 200
  8. 370

04Product Uses

  • Electrical cabinets & enclosures

    Panels, doors, frames and covers in thin and medium sheet.

  • General sheet metal fabrication

    Brackets, channels, machine covers and boxes in daily job-shop production.

  • Stainless steel & kitchen equipment

    Stainless panels and housings where consistent angles matter.

  • Door frames, elevator & HVAC parts

    Repeated profiles for building and ventilation components.

See all applications

05Operate Guide

  1. Check system and load

    Confirm your upper clamp is Amada type and keep the bending force below 35 T/m for this punch.

  2. Clean before clamping

    Wipe the tang, the clamp and the die seat; install segments with the same orientation.

  3. Choose the die opening

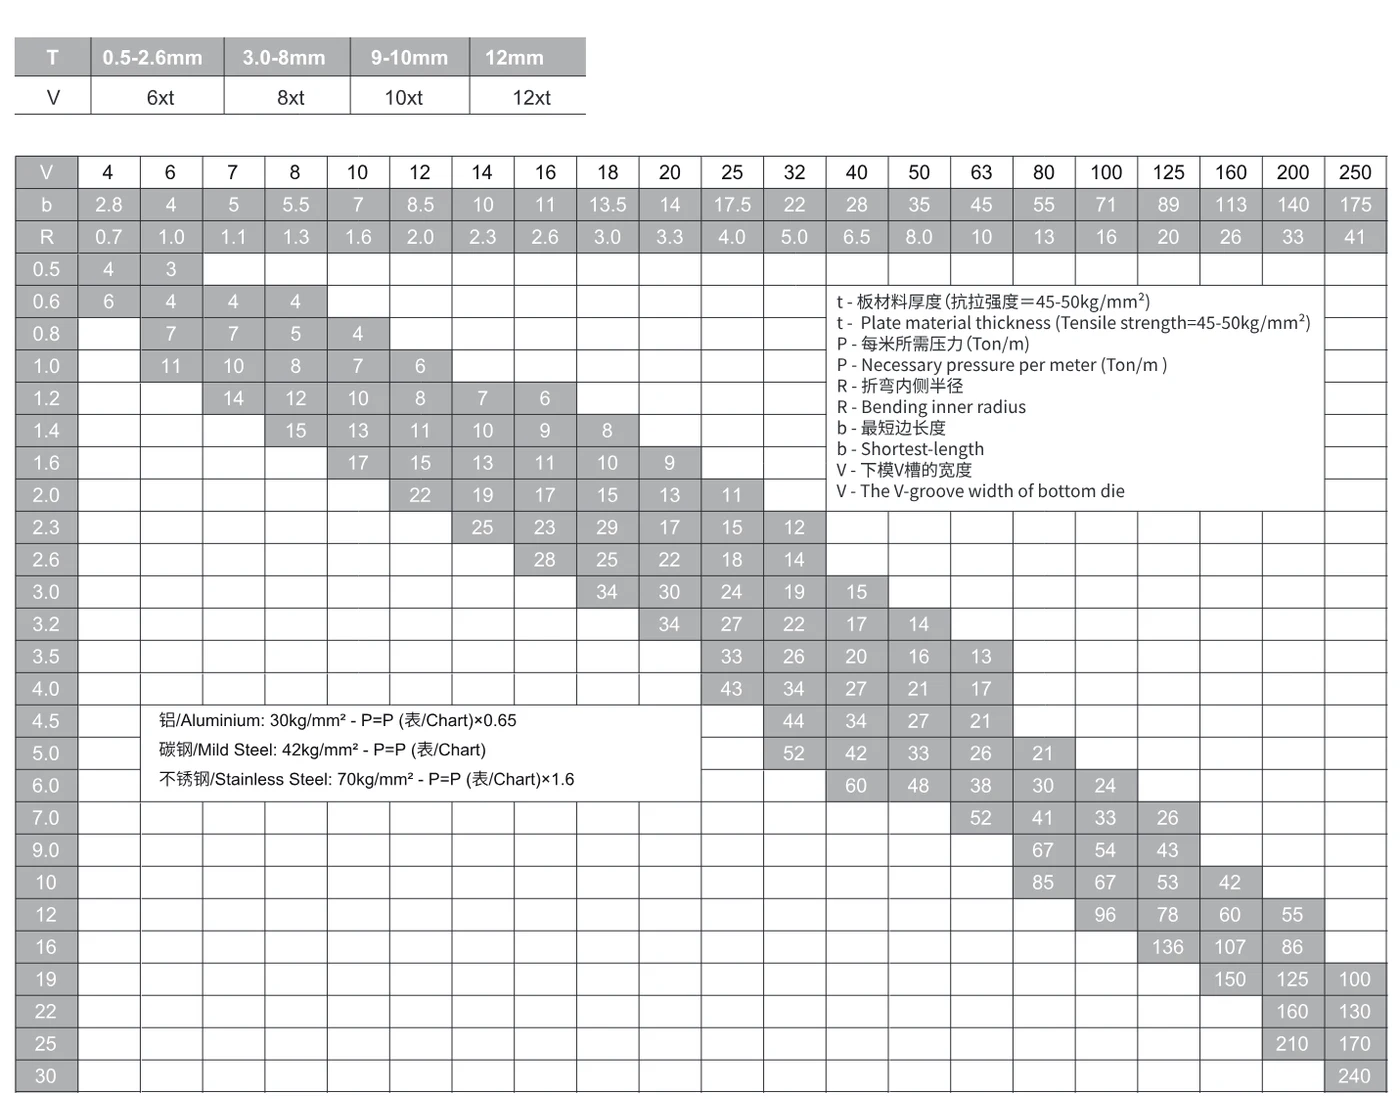
    Select the V opening from the sheet thickness — about 6 × t up to 2.6 mm, 8 × t from 3 to 8 mm.

  4. Clean, oil and store

    After use, clean and oil the tools and store them in a tooling cabinet to protect the working edges.

07FAQ

Are you a manufacturer or a trading company?

We are a manufacturer. The tools are designed, machined, heat treated, ground and inspected in our own factory in Ma'anshan, Anhui, China.

Will this punch fit my press brake?

It is made for press brakes with an Amada-type tooling system. Send us the brand and model of your machine and we confirm the clamping before quoting.

When can you ship after payment?

Standard products in stock usually ship in 3–7 days. Non-standard tools take 25–30 days; the making time of this punch is 25–30 days.

Can you put my brand name (logo) on the tools?

Yes. For OEM / ODM orders the MOQ is one piece, with a minimum order amount of USD 1,000.

Can you provide a sample to test?

Sure — tell us the profile and length you want to test and we will quote the sample.

How do you guarantee the quality?

If a quality problem is confirmed within 3 months of receiving the goods, we replace the tool free of charge. We hold an IQNET / CQM ISO 9001 certificate and have more than 20 years of production experience.

Contact us

Have a Drawing? Let's Build Your Tooling.

Tell us your press brake model, material, thickness and bend angle — or simply send a drawing. Our engineers reply within 24 hours with a recommendation and a quote.

    Request a Quote